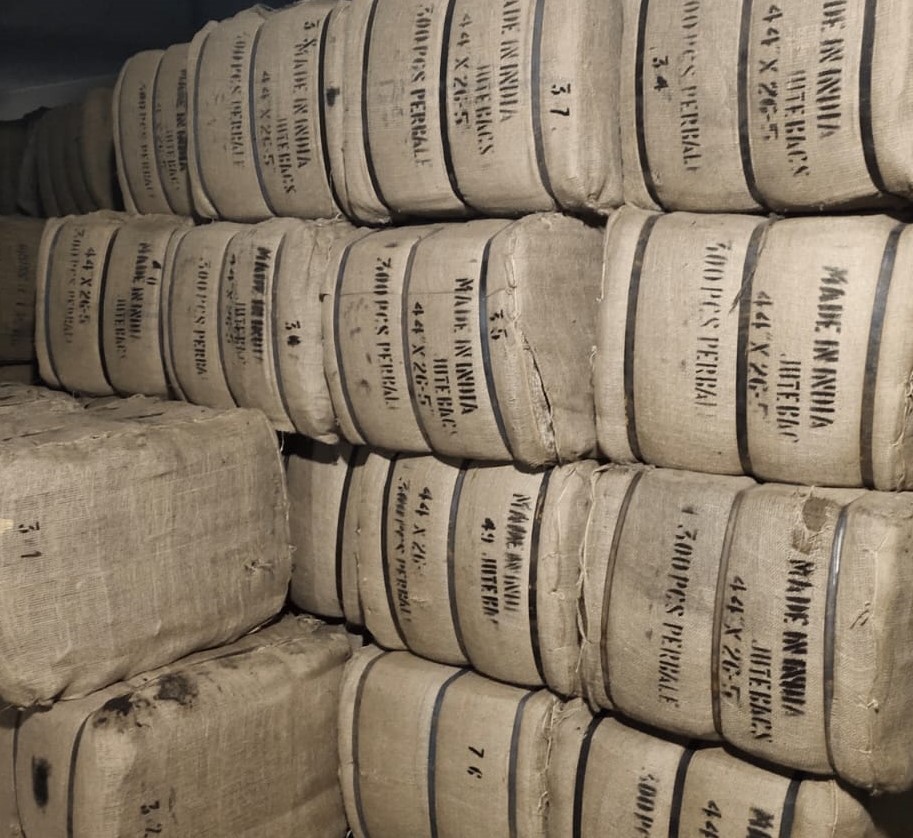
Hydro-carbon free (HCF) jute bags produced using Rice Bran Oil (RBO) and VOC technology, conforming to IJO 98/01 and IOCCC.
High-tensile PP Woven (45-205 GSM) and BOPP laminated bags offering photorealistic multicolour printing.
Hermetic vacuum packaging bags with EVOH oxygen barriers ensuring up to 2 years shelf life for sensitive products.
Packaging is far more than containment — it is the final line of defense in preserving product quality, safety, and commercial value from origin to end consumer. The right packaging solution protects against moisture, contamination, oxidation, and physical damage throughout the handling, storage, and transit process, while also enabling compliance with international food safety standards and buyer specifications.
We offer a comprehensive and versatile range of industrial and food-grade packaging solutions tailored to the specific requirements of agricultural and bulk commodity exports. Whether the commodity is a fine grain requiring breathable natural fibre, a processed kernel demanding hermetic vacuum protection, or a bulk material needing high-tensile synthetic strength, we have a packaging solution engineered to perform. All our packaging materials are sourced from reliable, quality-certified manufacturers and are available with options for custom printing, sizing, and food-grade compliance documentation.
Our jute sacking bags are manufactured from high-quality sacking fabric, available in plain and twill weaves. Commonly used for cement, sugar, grains, and other bulky items, jute bags are superior to synthetic alternatives in being biodegradable and breathable.
For food commodities such as cocoa, coffee, grains, and potatoes, we offer hydro-carbon free (HCF) food-grade jute bags produced using Rice Bran Oil (RBO) and Vegetable Oil Treated (VOC) technology, fully conforming to IJO 98/01 and IOCCC international specifications. Food-grade certificates issued by Cotecna/SGS are provided with each shipment, and these bags are approved by leading buyers in Europe, Africa, and Latin America.
PP Woven Sacks are among the toughest and most versatile packaging options available, widely used in the sugar, grain, milling, and food industries. Manufactured from polypropylene woven fabric, these bags offer superior strength, flexibility, and durability and are an excellent solution for packing 30-50 KG of dry material.
We manufacture a full range of laminated paper bags for chemicals, fertilisers, sugar, food grains, and similar products - in Open Mouth Sewn Bottom, Open Mouth Block Bottom, Valve Sacks, Polythene Lined, Bleached or Brown Kraft, and Gusseted configurations, printed up to 3 colours.
Vacuum bags are available in a 5-layer structure that ensures complete product protection from damage, moisture, and oxidation.
Consult our packaging engineers for certified bulk sacks, vacuum bags, and technical barrier solutions.